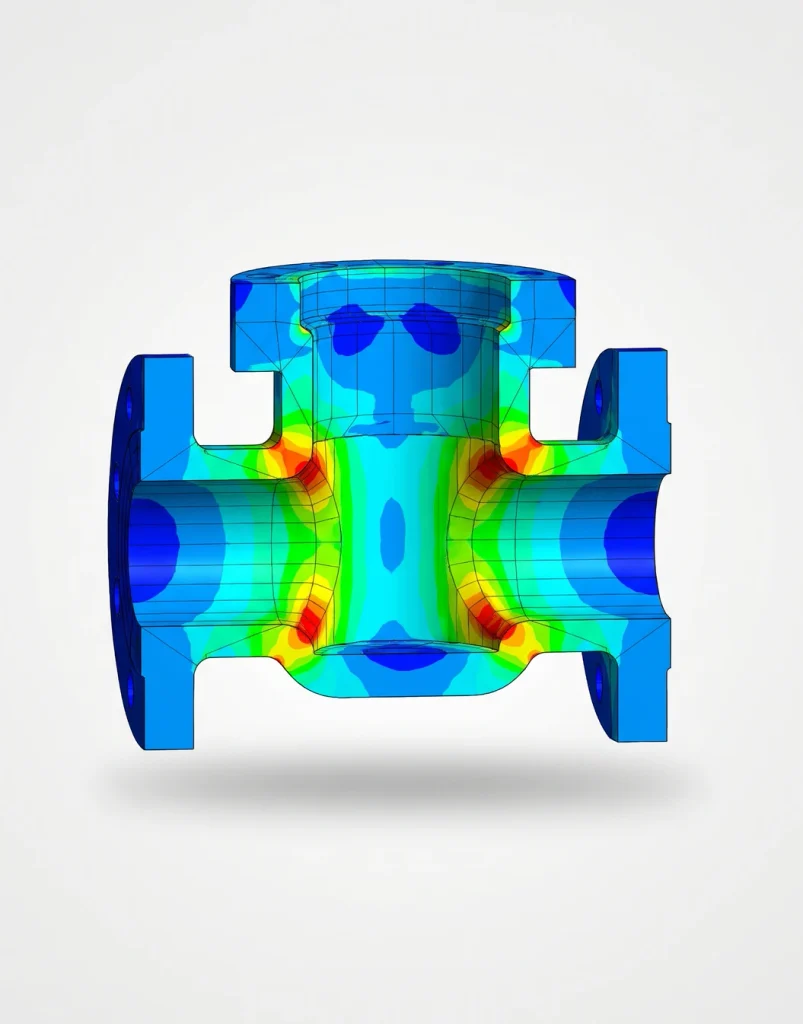
Torque specs on a bolted flange look precise — “450 ft·lbf, three passes, star pattern” — but the number behind that spec is built from a chain of assumptions, and the weakest link in that chain is almost always friction, not the bolt itself. Our Flange Bolt Torque calculator walks through that chain explicitly so you can see where the uncertainty actually lives.
Why torque is a proxy, not the goal
What a bolted joint actually needs is preload — the clamping tension holding the flange faces together against internal pressure and external loads. Torque is just the easiest thing to measure with a wrench in the field, so it’s used as a stand-in for preload. The relationship between the two is the classic short-form equation:
T = K × D × Fwhere T is applied torque, D is the nominal bolt diameter, F is the resulting bolt tension (preload), and K is the nut factor — a single number that lumps together thread friction, nut-face friction, and thread geometry effects. It’s a convenient equation. It’s also the reason torque-based tightening is a blunt instrument: K is not a material property, it’s a condition of the joint on that particular day.
Step 1 — size the bolt: tensile stress area
Before torque enters the picture at all, the calculator sizes the bolt itself. The load-carrying cross-section of a threaded fastener isn’t its nominal diameter — the threads cut material away — so engineering practice uses the standard tensile stress area:
At = (π/4) × (D − 0.9743/n)²where n is threads per inch. This is the same formula behind published UNC/UNF stress-area tables (Shigley, ASTM) — the calculator computes it live rather than looking it up, so it works for standard sizes and custom pitches alike.
Step 2 — set the target load
With At known, the target bolt load is a chosen percentage of the bolt material’s minimum yield strength (SMYS):
F = target% × SMYS × AtASME PCC-1 Appendix O guidance typically lands in the 40–70% of SMYS range: high enough to hold a reliable seal margin against pressure and thermal cycling, low enough to leave headroom before yield and to avoid stress-relaxation problems at gasket loading. 50% is a common, conservative starting point for general service.
Step 3 — convert load to a wrench setting
This is where K comes back in. Typical starting values:
- Dry / as-received threads: K ≈ 0.20
- Lightly lubricated: K ≈ 0.18
- Lubricated or plated: K ≈ 0.15
- Anti-seize / moly paste: K ≈ 0.12
Notice the spread: the same target preload can call for a torque anywhere from roughly 0.12 to 0.20 × D × F depending purely on what’s on the threads that day. Swap in the wrong K — assume “lubricated” when the fitter actually ran it dry — and the applied torque can undershoot or overshoot the intended preload by 30% or more, even though the wrench read exactly the number on the spec sheet.
Worked example
A 3/4″-10 UNC ASTM A193 B7 stud (SMYS = 105,000 psi), target 50% of SMYS, lightly lubricated (K = 0.18):
- At = (π/4) × (0.75 − 0.9743/10)² = 0.334 in²
- F = 0.50 × 105,000 × 0.334 = 17,559 lbf
- T = 0.18 × 0.75 × 17,559 = 2,370 in·lbf ≈ 198 ft·lbf
Run the same bolt dry (K = 0.20) instead of lubricated, and the torque needed for the same 17,559 lbf preload jumps to about 220 ft·lbf — a 10%+ difference from the lubrication condition alone, with the bolt size and target load unchanged.
What this method doesn’t cover
Torque-based tightening with a generic K-factor is a preliminary screening tool, not a substitute for a bolted-joint design package. It doesn’t check gasket seating stress or blowout, bolt spacing and pattern, elastic interaction between bolts as they’re sequentially tightened, or the actual flange rating (ASME B16.5 / API 6A) for the service pressure and temperature. For a leak-critical joint, cross-check against a published torque table for the specific flange class and gasket, or use a more accurate tightening method — turn-of-nut, bolt elongation measurement, or ultrasonic tensioning — that measures preload more directly than torque can.
Try it yourself with the Flange Bolt Torque calculator — swap bolt sizes, materials, and lubrication conditions to see how sensitive the final torque number really is.